> For the complete documentation index, see [llms.txt](https://wiki.polymaker.com/llms.txt). Markdown versions of documentation pages are available by appending `.md` to page URLs; this page is available as [Markdown](https://wiki.polymaker.com/polymaker-wiki/polymaker-wiki-ko/undefined-1/common-printing-issues/curling-of-layers-and-angles.md).
# 레이어 및 각도 말림
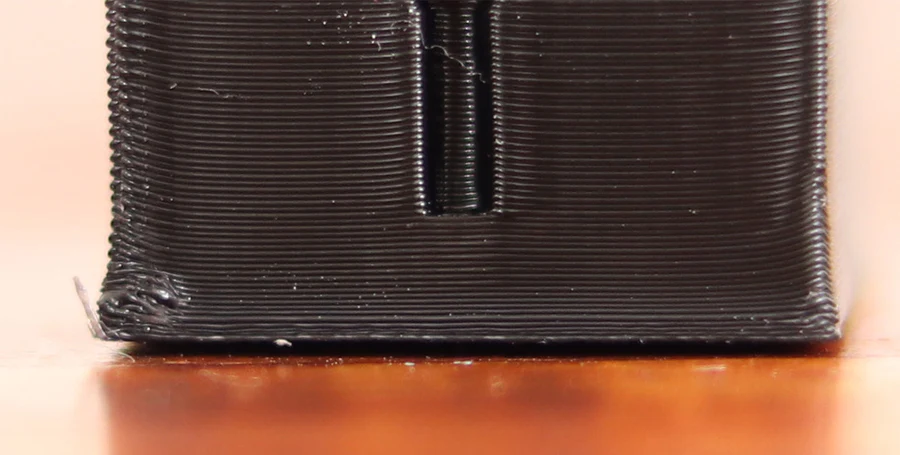
이 문제는 휨처럼 보일 수 있지만, 실제로는 출력물이 베드에서 들리는 것이 아니라 **개별 레이어가 위로 말리는 현상**입니다.
그래서 [워핑](broken://spaces/KnR2KiZmkGXTiYikBIdN/pages/XIDT1uRZyk2PJc2Hy6v7) 해결책과는 정반대인 경우가 많습니다.
### 액티브 쿨링 팬 켜기
PLA에서 팬이 없거나 팬 속도가 부족하면 레이어 말림이 자주 생깁니다.
PLA는 강제 냉각이 잘 맞는 소재라, 보통 \*\*첫 레이어 이후 팬 100%\*\*가 가장 무난합니다.

첫 레이어는 팬을 끄고, 두 번째 레이어부터 올리는 방식이 일반적입니다.
### 주변 온도도 확인
PLA는 유리전이온도가 낮아, 너무 따뜻한 챔버 안에서는 더 쉽게 말릴 수 있습니다.
그래서 PLA는 완전 밀폐 챔버보다 **개방된 환경**이 더 유리한 경우가 많습니다.
### 레이어가 식을 시간이 부족함
작은 탑이나 뾰족한 형상처럼 같은 위치에 레이어가 빠르게 계속 쌓이면, 이전 레이어가 식기 전에 다음 레이어가 올라와 말림이 생길 수 있습니다.
그래서 `Minimum Layer Time` 설정이 중요합니다.

대부분 소재는 **3–5초** 정도면 충분합니다.
`Lift Head` 기능이 있으면 정지 중 노즐이 출력물 위에 머무는 열도 줄일 수 있습니다.
### 레이어 높이와 온도
너무 얇은 레이어는 더 쉽게 말립니다.
이 경우 레이어 높이를 약간 높이거나 속도를 조정하는 것이 도움이 될 수 있습니다.
노즐 온도도 권장 범위 안에서 약간 낮춰 보는 것이 좋습니다.
특히 작은 노즐과 얇은 레이어 조합일수록 더 그렇습니다.
### 서포트와 수분도 점검
급한 오버행은 서포트를 더 일찍 쓰는 편이 좋습니다.
또 위 조정을 해도 계속 말린다면 필라멘트 수분도 확인하세요.
## 요약
* 소재가 요구한다면 액티브 쿨링 팬을 켜세요. PLA는 첫 레이어 이후 **100% 팬**이 가장 무난합니다.
* 주변 온도가 출력 소재의 유리전이온도에 가까워지지 않도록 하세요. PLA는 완전 밀폐형 장비에서 불리할 수 있습니다.
* Cura의 `Minimum Layer Time`은 최소 **3초** 이상으로 두어 각 레이어가 식을 시간을 확보하세요.
* 낮은 레이어 높이는 강성이 약하므로, 레이어 높이나 출력 속도를 조금 올리면 도움이 될 수 있습니다.
* 특히 작은 노즐과 낮은 레이어 높이 조합이라면 노즐 온도를 약간 낮춰 보세요.
* 액티브 쿨링을 쓰기 어려운 소재라면 서포트를 켜고 서포트 생성 각도를 더 보수적으로 잡으세요.
* 위 방법을 모두 시도했는데도 계속 말린다면 필라멘트 수분도 점검하세요.
{% embed url="" %}
---
# Agent Instructions
This documentation is published with GitBook. GitBook is the documentation platform designed so that both humans and AI agents can read, navigate, and reason over technical content effectively. Learn more at gitbook.com.
## Querying This Documentation
If you need additional information that is not directly available in this page, you can query the documentation by asking a question.
Perform an HTTP GET request on the following URL with the `ask` and `goal` query parameters:
```
GET https://wiki.polymaker.com/polymaker-wiki/polymaker-wiki-ko/undefined-1/common-printing-issues/curling-of-layers-and-angles.md?ask=&goal=
```
`ask` is the immediate question: it should be specific, self-contained, and written in natural language.
`goal` is what the user is ultimately trying to achieve, the reason they need the answer. Sharing it helps GitBook give you a better, more relevant answer. A goal is most helpful when it describes the outcome the user wants rather than restating the question. For example, with `ask=how do I create an API token`, a goal like `automate deployments from our CI pipeline` lets GitBook tailor the answer to that use case.
The response will contain a direct answer to the question and relevant excerpts and sources from the documentation.
Use this mechanism when the answer is not explicitly present in the current page, you need clarification or additional context, or you want to retrieve related documentation sections.